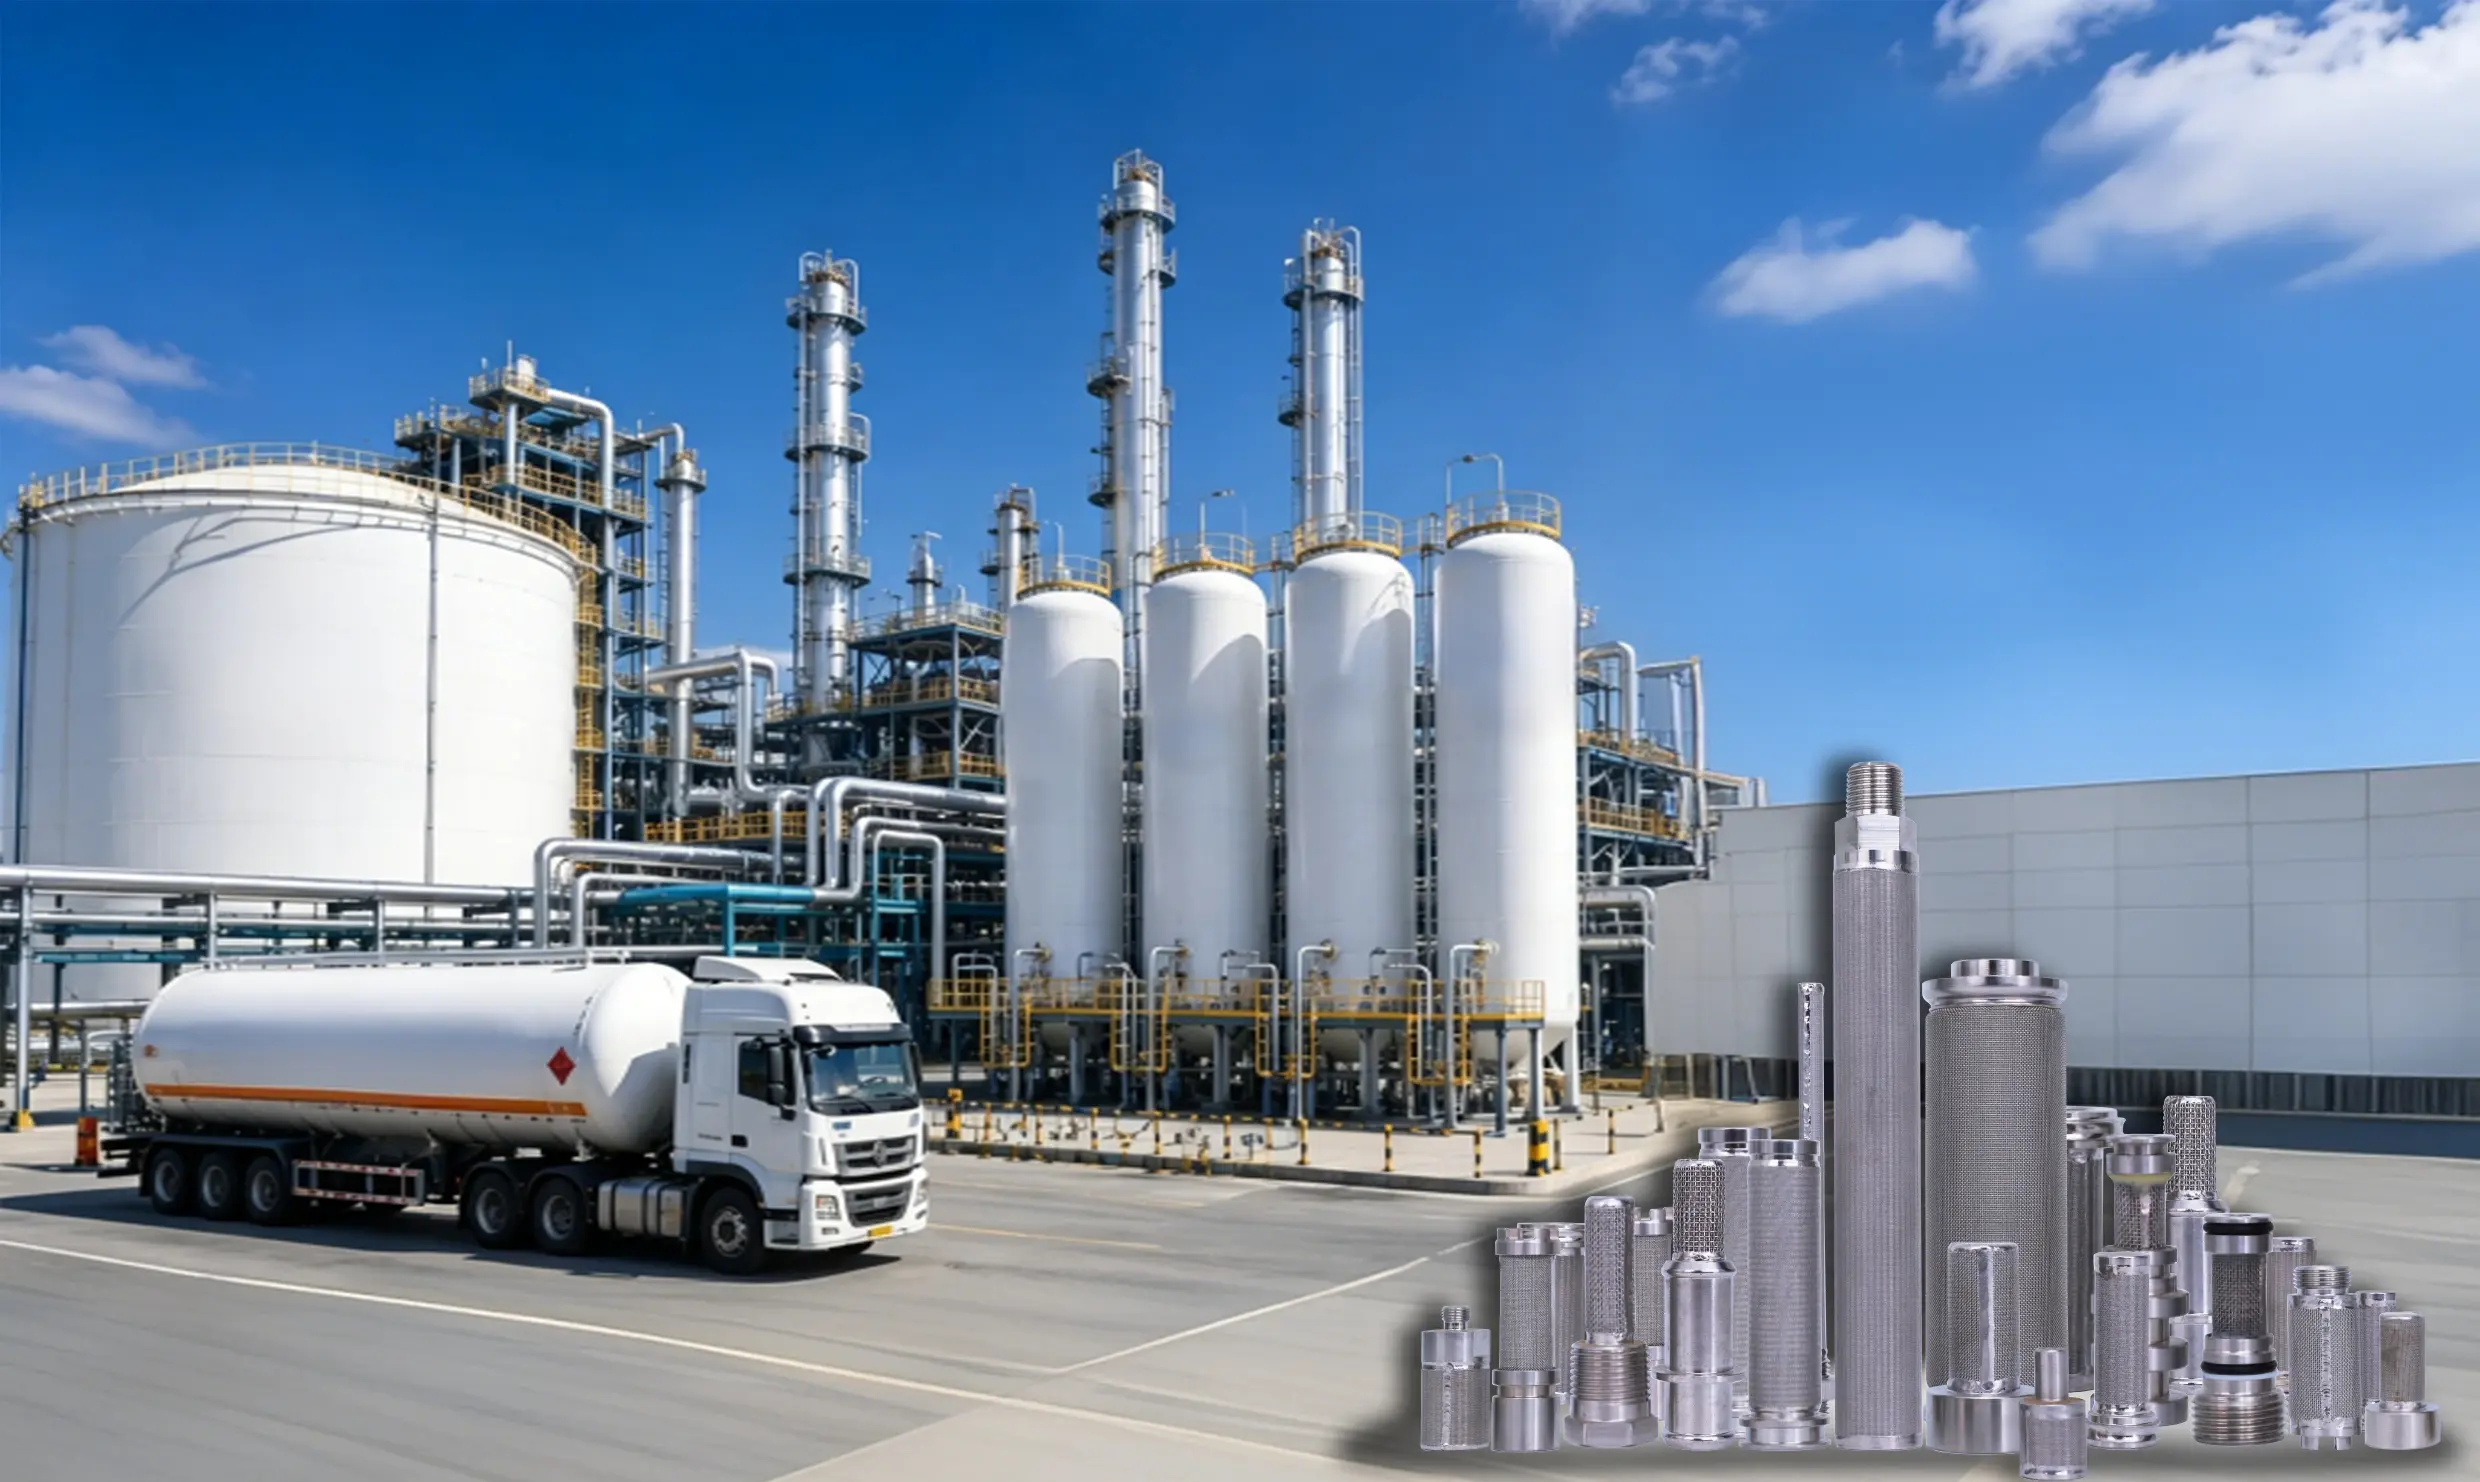
Sintered Mesh Filters for Natural Gas & Industrial Gas Industry
The Critical Process Filter Element (CPFE) for natural gas, LNG, CNG, hydrogen refueling, PSA N₂ / O₂ / H₂, air separation units (ASU), semiconductor UHP gas and BF gas service.
Industry Characteristics
Why Natural Gas & Industrial Gas Demands CPFE-Grade Sintered Mesh
Gas service is unique: the product itself is the asset, downstream equipment is critical, and contamination is unforgiving. Pressures range from 10 to 900 bar. Flows from thousands to hundreds of thousands of Nm³/h. Temperatures from −196 °C to 600 °C — sometimes within a single plant. And the filter must withstand all of it while delivering permanent micron rating and zero media migration. That’s why every major gas plant classifies sintered mesh as a Critical Process Filter Element, not a consumable.
Ultra-High Gas Purity
99.999% – 99.99999% (5N–7N) — sintered mesh delivers permanent micron rating without media drift.
Ultra-High Pressure
10–900 bar including hydrogen refueling at 350–900 bar — 5-7 layer construction holds.
Cryogenic Service
−163 °C LNG, −196 °C ASU — stainless steel retains excellent toughness at cryogenic temperature.
High-Temperature Gas
300–600 °C BF gas, process gas — 310S sintered mesh retains structure.
Online Back-Flush
Diffusion-bonded structure tolerates years of automatic backwash without drift.
Sour & Acid Gas
H₂S, CO₂ — 904L and Hastelloy C-276 per NACE MR0175 / ISO 15156.
Application Coverage
14 Typical Gas Service Applications — Equipment, Conditions & Recommended Structure
From long-distance natural gas pipelines and city gates, to LNG receiving and liquefaction, CNG and hydrogen refueling stations, PSA N₂ / O₂ / H₂ generation, air separation units, ammonia & methanol synthesis, semiconductor specialty gas and BF gas. Each maps to a specific sintered mesh structure and material.
← Scroll horizontally to view all columns →
| Application Equipment | Install Location | Protected Equipment | Working Conditions | Contaminants | Customer Pain Point | Consequence Without Filter | Recommended Structure |
|---|---|---|---|---|---|---|---|
| Natural Gas Long-Distance Pipeline | Pipeline Filter | Compressors, regulation valves | 20–120 bar | Rust, weld slag, dust | Valve wear | Transmission system fault | 5-Layer 316L Sintered |
| Natural Gas City Gate | Inlet Filter Separator | Pressure regulation equipment | High-flow service | Rust, droplets | Regulator seizure | Supply interruption | Sintered Mesh |
| LNG Receiving Terminal | BOG Gas Filter | Compressors | −163 °C ~ 50 °C | Ice crystals, rust | Compressor damage | LNG system shutdown | 316L Cryogenic Sintered |
| LNG Liquefaction Unit | Process Gas Filter | Cryogenic exchanger, compressor | Cryogenic service | Metal particles | Exchanger plugging | Efficiency drop | 316L Sintered |
| CNG Refueling Station | Compressor Inlet Filter | Compressor | 200–350 bar | Rust, dust | Compressor wear | Higher maintenance cost | High-Pressure Sintered |
| PSA Nitrogen Generator | Product Gas Filter | Nitrogen system | 5–13 bar | Molecular sieve dust | Nitrogen purity drop | Off-spec product | Sintered Mesh |
| PSA Oxygen Generator | Oxygen Filter | Oxygen system | High-purity O₂ | Molecular sieve dust | Oxygen contamination | Safety risk | Degreased 316L Sintered |
| Air Separation Unit (ASU) | Product Gas Filter | O₂, N₂ system | Ultra-high purity | Sub-micron particles | Gas purity drop | Product scrap | Electropolished Sintered |
| Hydrogen Production | Hydrogen Filter | Compressor, H₂ storage | High-purity H₂ | Catalyst powder | Compressor wear | H₂ purity drop | 316L / Hastelloy Sintered |
| Ammonia Synthesis | Process Gas Filter | Synthesis tower catalyst | High-temp / high-pressure | Rust, catalyst powder | Catalyst deactivation | Lower conversion rate | Sintered Mesh |
| Methanol Plant | Syngas Filter | Catalyst bed | 50–100 bar | Metal particles | Catalyst plugging | Lower output | 5-Layer Sintered |
| Hydrogen Refueling Station | Hydrogen Filter | Refueling dispenser | 350–900 bar | Metal particles | Refueling gun fault | Safety risk | HP 7-Layer Sintered |
| Semiconductor Electronic Gas | UHP Gas Filter | Wafer fab equipment | Ultra-clean service | Sub-micron particles | Chip defects | Product scrap | Electropolished Sintered |
| BF Gas System | Gas Filter | Fans, compressors | High-temp dust-laden | Coke fines, iron-oxide dust | Fan wear | Shutdown maintenance | 310S Sintered |
Material Selection
Material Selection Guide — Gas Service to Recommended Construction
Construction is matched to gas chemistry, target purity and operating envelope. Use this as a starting reference; we tailor per fluid analysis & NACE / API requirements.
| Service Environment | Recommended Material | Rationale |
|---|---|---|
| General natural gas | 316L Sintered | Industry-standard configuration. |
| LNG cryogenic system | 316L Cryogenic Sintered | Resistance to low-temperature embrittlement. |
| High-pressure natural gas | 7-Layer 316L Sintered | Maximum mechanical strength. |
| Sour natural gas | 904L Sintered | Resistance to sulfide stress corrosion. |
| Acid gas (H₂S + CO₂) | Hastelloy C-276 | Maximum corrosion resistance. |
| Hydrogen system | 316L / Hastelloy | Hydrogen embrittlement resistance. |
| High-purity oxygen system | Degreased 316L Sintered | Oxygen-safety requirement (ASTM G93 Level B). |
| Semiconductor specialty gas | Electropolished 316L Sintered | Ultra-high purity (UHP) compliance. |
| BF gas / High-temp gas | 310S Sintered | High-temperature stability above 600 °C. |
| Automatic backwash system | 5-Layer Sintered | Long-life cycling under pulse backwash. |
Operating Conditions
Why Sintered Mesh — Mapped to Gas Service Conditions
| Condition Type | Working Conditions | Why Stainless Steel Sintered Mesh |
|---|---|---|
| High-Pressure Gas | 50–900 bar | Sintered mesh has extreme mechanical strength. |
| Ultra-High-Purity Gas | 99.999%+ | Stable pore size, zero fiber shedding. |
| Cryogenic Service | −196 °C | Stainless steel retains excellent low-temperature toughness. |
| High-Temperature Service | 300–600 °C | All-metal construction tolerates sustained heat. |
| Online Pulse Backwash | Automatic backwash filter | Sintered mesh tolerates indefinite back-flush cycling. |
| Corrosive Gas | H₂S, CO₂ | 904L and Hastelloy material options. |
| Continuous Operation | 24 h continuous duty | Multi-year service life between change-outs. |
| Hazardous Area | Explosion-rated zones | All-metal construction is intrinsically safe. |
Customer Concerns
Top 5 Questions from Gas Industry Customers
1. Why is sintered mesh classified as a critical process filter in gas service?
add
In natural gas, LNG and industrial gas plants, the gas product is high-value and downstream equipment — compressors, catalyst beds, expanders, cryogenic exchangers, hydrogen refueling dispensers — is mission-critical. A single particle can destroy a compressor impeller or poison a catalyst bed worth millions. Sintered mesh delivers permanent micron rating, zero fiber migration, and the strength to survive 900-bar hydrogen refueling and −196 °C cryogenic ASU service. That’s why every major gas plant treats it as a Critical Process Filter Element (CPFE), not a consumable.
2. What’s special about 900-bar hydrogen refueling station filtration?
add
Hydrogen refueling at 350–900 bar is one of the most demanding filtration services in industry. SINFT 7-layer high-strength 316L (and 904L for severe service) sintered mesh elements deliver permanent 1–3 µm micron rating with zero fiber shedding at 900 bar — protecting the dispenser, fuel cell stack and Type IV storage vessel. Hydrogen embrittlement-resistant material selection is critical.
3. Can SINFT supply sintered mesh for LNG cryogenic service?
add
Yes. 316L sintered mesh retains excellent toughness at −163 °C (LNG) and even −196 °C (ASU liquid air). We supply BOG (boil-off gas) filters, cold-box pre-filters for liquefaction, and cryogenic gas filters for ASU service. The diffusion-bonded multi-layer construction has no fasteners, gaskets or polymer parts that would fail at cryogenic temperature.
4. Which material for high-purity (99.999%+) gas service?
add
99.999% to 99.99999% (5N to 7N) purity requires electropolished 316L sintered mesh with degreased finish for oxygen safety. For semiconductor specialty gases (Cl₂, HCl, HBr, F₂ etc.) Hastelloy C-276 is recommended. Degreasing per ASTM G93 Level B available on request for oxygen service.
5. What about sour gas (H₂S + CO₂) and acid gas service?
add
For sour natural gas with H₂S and CO₂, 904L sintered mesh is the standard — resists sulfide stress cracking and chloride pitting. For severe sour service (high H₂S concentration, high temperature, brine-bearing), Hastelloy C-276 is recommended. Material is matched per NACE MR0175 / ISO 15156 requirements.
Related Products & Applications
Explore Related Solutions
Sintered Mesh Filter
Back to the full product overview, specs and downloads.
Pleated · Compressed Air & Gas
Bulk-flow ISO 8573 compressed air & PSA service.
Pleated · Oil & Gas
Upstream gas separator, LNG and offshore service.
Sintered · Petrochemical
FCC, hydrocracking, HDS and polymer melt service.
Request a Quote — Natural Gas & Industrial Gas Sintered Mesh
Tell us your gas service (natural gas, LNG, CNG, PSA N₂/O₂/H₂, ASU, hydrogen refueling, semiconductor UHP…), pressure, temperature, flow rate and required purity (5N–7N) — our engineering team replies with a tailored specification within 24 hours.