A new stainless steel filter can arrive with the correct dimensions and paperwork yet still need a closer look before installation. A loose fiber inside the outlet, an unexplained film on a sealing face or a torn protective bag can change the acceptance decision. This filter element surface cleanliness inspection guide helps purchasing, quality and maintenance teams check what matters without treating a bright metal finish as proof of cleanliness.
What Should a Filter Element Surface Cleanliness Inspection Cover?
Check the packaging, accessible media surfaces, seams, end fittings, inner passage and sealing areas against the cleanliness requirement agreed for the intended service. Record visible contamination and any inspection limits. Where particle or residue limits apply, use the specified, suitable verification method; a visual check alone cannot establish a quantitative cleanliness level.
Before releasing an element, answer four questions:
- Does the received condition match the packaging and cleanliness requirements?
- Are there visible particles, fibers, films, moisture or unexplained deposits?
- Can the relevant surfaces actually be inspected with the chosen method?
- Is the evidence sufficient for this installation, or is further review required?
This is a separate decision from confirming material grade, dimensions or filtration rating. A filter can meet those requirements while still carrying contamination introduced during production, inspection, packing, transport or handling.
Start with the Service Requirement, Not a Universal Cleanliness Grade
“Clean before delivery” is difficult to verify unless the order explains what clean means. For one installation, the requirement may be a defined visual condition and protected packaging. Another may require a documented particulate assessment or a separately specified residue limit. These are different acceptance tasks.
For a hydraulic filtration application, consider where an introduced particle could travel during installation and startup. The element's filtration rating does not authorize leaving debris on its downstream surfaces. A particle already inside the clean-side passage may enter the system without crossing the intended filtration layer.
Identify the contaminant of concern: loose metal particles, packaging fibers, machining residue, cleaning-agent residue or another process-specific substance. Then define the inspected surfaces, method, sampling basis, criteria and decision authority. Do not copy limits from an unrelated component simply because both are stainless steel.
An operating-fluid cleanliness target is also not, by itself, a complete acceptance specification for a dry component. The inspection object, collection method and reporting basis need to be defined for the element being purchased.
Inspect the Package Before Opening It
Photograph the received package and label before removing protection. Check for punctures, open seams, crushed supports, displaced caps, moisture and loose packaging material. Distinguish damage to the outer transport carton from damage to the protective barrier around the element.
A dented carton does not automatically prove contamination. An intact outer carton does not prove that an inner bag remained sealed. Record the condition that can actually be established, including whether the relevant protective barrier has been compromised.
Unpack in a suitable receiving area with clean handling materials. Keep the element away from grinding dust, carbon-steel swarf and dirty benches. Handle robust fittings where practical and avoid touching functional surfaces unnecessarily. Gloves and tools must be suitable for the intended cleanliness requirement; visibly clean gloves can still transfer unwanted material.
Keep packaging and identity information associated with the part while reviewing a concern. If a quantitative as-received cleanliness assessment is required, follow the agreed handling plan before opening or touching the item. A casual receiving inspection can change the condition that a later assessment was supposed to measure.
Check the Places Where Contamination Can Be Missed
A quick look at the outer cylinder leaves important areas unexamined. Plan access around the actual construction and intended flow path. Identify the downstream side from the drawing or installation information rather than assuming that the inside of every cartridge is the clean side.
| Inspection area | What to look for and what to record |
|---|---|
| Accessible media surface | Loose particles, fibers, deposits or visible film; note any guard or layer that blocks the view. |
| Pleat valleys and guarded areas | Material lodged between folds or behind protection; record areas that cannot be inspected directly. |
| Seams and welded transitions | Attached debris, loose residue and deposits around joints; distinguish contamination from a possible construction defect. |
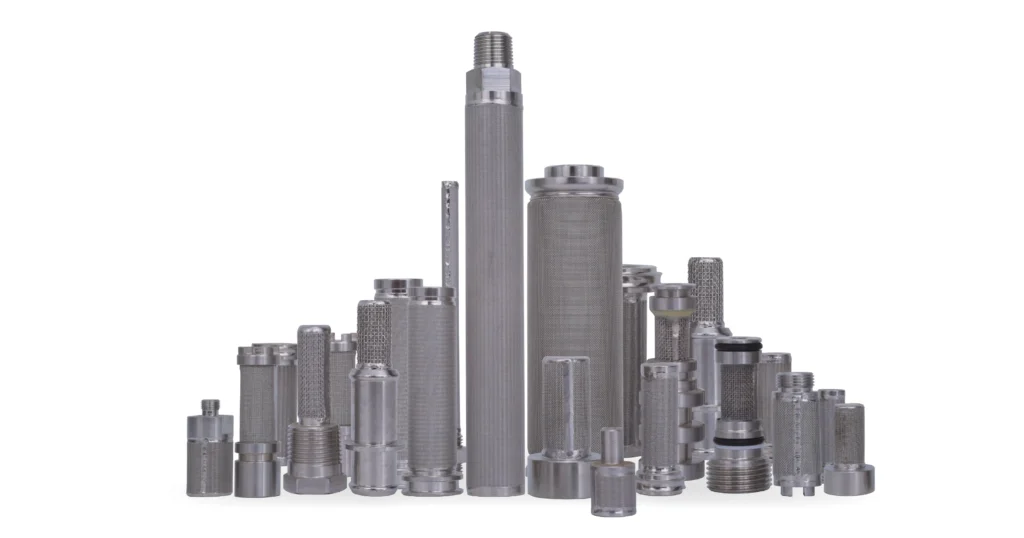
| End caps, threads and recesses | Trapped machining debris, packaging fragments or unapproved lubricant; check against the intended assembly condition. |
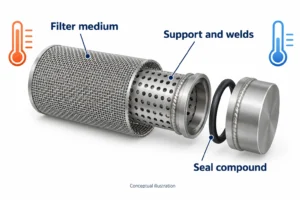
| Inner passage and support tube | Loose material on accessible internal surfaces and at the outlet; do not infer hidden-surface cleanliness from a clear opening. |
| Sealing faces and grooves | Debris, films, damage or foreign material that could affect seating; identify approved assembly lubricant separately. |
| Caps, bags and contact packaging | Moisture, particles or fibers that could transfer back to the element after inspection. |
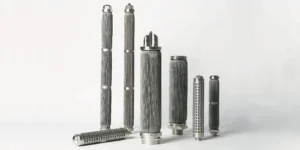
For sintered mesh filter elements, an outer protective layer can conceal the finer filtration layer. Visible surface condition does not establish the condition throughout a multilayer porous wall.
For pleated filter cartridges, fold spacing, guards, cores and end-cap transitions affect access. Do not force a probe between pleats or dismantle an assembly merely to obtain a better view. Agree an alternative inspection approach where access is inadequate.
Use enough suitable lighting to distinguish a deposit from a shadow, and record the viewing conditions when they affect a decision. Close-up photographs help communicate a location and appearance. They do not provide a reliable particle-size measurement unless the imaging method and scale support that measurement.
Separate Particles, Films, Moisture and Surface Discoloration
Loose particles and fibers are one category of concern. An oily or detergent-like film is another. A particle assessment does not automatically answer whether an unwanted chemical residue is present. Likewise, a residue assessment may not establish the size or number of loose particles.
Moisture deserves its own review. It may be related to rinsing, packaging or environmental exposure, but appearance alone cannot identify its source or composition. Record where it is found and compare it with the specified delivery condition. Do not assume that clear liquid is harmless water or that all supplied elements must have the same dry-delivery requirement.
Discoloration also needs interpretation. A dark spot, heat tint or stain is not automatically loose contamination, and a bright surface is not proof of an acceptable chemical condition. Where the appearance is unexplained or conflicts with the specification, obtain a technical assessment rather than declaring it harmless or identifying corrosion from a photograph alone.
Approved assembly lubricant may be intentional on a seal or fitting. Confirm its identity, location and compatibility against the order. A generic “oil-free” instruction can conflict with an approved assembly requirement unless the surfaces and permitted materials are clearly defined.
Passivation and Cleanliness Answer Different Questions
A passivation record does not establish the current cleanliness of an element after shipping and unpacking. Surface treatment, subsequent rinsing, handling and packaging form a sequence; contamination can be introduced after an earlier operation was completed.
The public scope of ASTM A380/A380M-25 addresses cleaning and surface-treatment practices for stainless steel, with procedures selected by purchaser–supplier agreement. It recognizes the importance of geometry that permits cleaning and removal of cleaning solutions. Referencing the practice does not establish that every listed method is appropriate for a particular porous assembly.
Our stainless steel filter element passivation guide explains the purchasing questions around that treatment. For installation acceptance, check the delivered condition and the required records separately. Do not use a passivation statement as a substitute for missing particulate or residue evidence.
When Visual Inspection Is Not Enough
Visual inspection is useful for finding accessible, observable concerns. Its limits include hidden layers, internal recesses, small particles and films that may not be apparent under the viewing conditions. “No visible contamination observed” is a narrower conclusion than “no contamination present.”
The public scope of ISO 16232:2018 concerns particulate-contamination assessment of road-vehicle components and systems. It excludes film contamination, non-quantitative checks such as visual or cloth-wipe assessment, and operating-fluid characterization. It also does not supply universal component cleanliness limits. Its automotive scope must be considered before specifying it for another application.
If a project requires quantitative particulate evidence, have the responsible specialists agree a suitable collection and analysis approach for the actual element. For a porous metal assembly, the method must address what can be collected from the relevant surfaces and whether the examination itself could release material from the medium or alter the assembly.
Ask how collection coverage, method background, sampling and the reporting basis will be controlled. Results expressed per element, per area or for a combined sample are not interchangeable without the necessary context. Background contamination from the examination process must not be silently attributed to the part.
For chemical-residue concerns, specify an appropriate assessment separately. A request for “a cleanliness test” does not identify the substance, method or acceptable result. Specialized analysis must be confirmed for the project; it should not be assumed to be part of every supplier's routine inspection package.
Avoid Turning an Inspection into Uncontrolled Cleaning
Finding debris often triggers an immediate attempt to wipe, blow or rinse it away. That can remove evidence, introduce another contaminant or push material farther into the porous structure. It can also change the condition before the supplier and buyer agree how to investigate it.
Do not rub an ordinary cloth across fine media as an improvised particle test. It may leave fibers, and its result cannot be treated as a quantified assessment. Similarly, shop compressed air or an unapproved solvent is not automatically suitable for a delivered filter assembly.
Where cleaning is authorized, use a process compatible with the medium, joints, seals and intended duty. Define what evidence will support reacceptance afterward. A better-looking surface alone may not answer the original concern.
If an apparent deposit may instead be a broken wire, damaged pore structure or joint defect, assess integrity as a separate issue. The filter pore and slot integrity inspection guide addresses that construction-focused question. Cleaning cannot be used to dismiss an unresolved physical defect.
A Practical Hold-and-Release Decision
The following examples are receiving decisions to adapt to the order, not universal rejection criteria. Use the agreed specification and the responsible technical authority for the final disposition.
| Received condition | Appropriate next step |
|---|---|
| Packaging intact; required checks and records acceptable | Record acceptance and preserve protection until controlled installation. |
| Outer carton damaged; inner protection apparently intact | Document both conditions and assess whether the defined barrier and inspection requirements remain satisfied. |
| Protective bag open, missing cap or unexplained moisture | Hold the affected item for review of exposure, delivery requirements and further inspection. |
| Loose fibers, chips or unidentified film on a functional surface | Photograph the location before disturbance; segregate and request a defined disposition. |
| Visual condition acceptable but required quantitative evidence absent | Obtain the specified evidence or authorized resolution before release. |
| Cleaning or rework authorized | Record the action, repeat the relevant acceptance checks and restore agreed packaging. |
Avoid mixing affected and accepted elements while a concern is being reviewed. Define the scope of the hold: one identified item, a package or a wider batch if the available evidence warrants it. One observed issue does not prove that every item is affected, but it may justify checking whether they shared the same exposure or process.
What Should the Inspection Record Contain?
A useful record connects observations to the part and the release decision. Include the part number and drawing revision, batch or serial reference where applicable, inspection date, inspector and applicable requirement. Identify whether the record covers each item or a defined sample.
Describe package condition, inspected locations, method and any inaccessible areas. Keep photographs associated with the correct item, with both a general view and a close view where useful. Record actual observations rather than a vague entry such as “appearance OK.”
Where quantitative or residue assessment was required, retain the method reference, sampling basis, results, units and acceptance criteria. State limitations and deviations that affect interpretation. A supplier declaration, a visual checklist and a detailed analytical report carry different information; request the document that answers the agreed question.
Finish with a clear disposition: accepted, held for review, rejected under the applicable requirement or released after an authorized corrective action. Record who approved the decision and what packaging or handling condition must be maintained afterward. This preserves traceability between the received condition and installation release.
Put Cleanliness and Packaging in the RFQ
Define the requirement before manufacture, especially when the part has deep folds, multiple layers, enclosed spaces or sensitive downstream duty. Retrofitting an undefined cleanliness requirement at delivery makes both inspection and acceptance harder.
Send the following information with the drawing or replacement sample:
- Working medium, application and the relevant contamination concern.
- Part configuration, intended flow direction and critical wetted or sealing surfaces.
- Required visual condition and any separately defined particulate or residue criteria.
- Inspection method, coverage and sampling requirements, where specified.
- Required records, identity links and approval of deviations.
- Packaging, permitted protective materials and delivery condition.
- Handling or installation restrictions that must be communicated with the shipment.
SINFT's confirmed capabilities include surface-cleanliness inspection and passivation-related inspection documentation, with the actual scope agreed for the order. Specific quantitative analyses, specialized cleaning qualifications or regulated-service requirements need separate confirmation. Do not infer them from a general inspection capability statement.
Use the custom filter manufacturer page for drawing-based supply and replacement requirements. For a current project, send the drawing, duty and proposed cleanliness criteria through the contact inquiry form. Agree what will be checked and delivered before the order is released.
Frequently Asked Questions
Does a passivation certificate prove that a filter element is clean?
No. A passivation record concerns a specified treatment and its documented scope. It does not automatically establish the element's current particulate condition, absence of residual films or condition after transport. Review the agreed cleanliness requirements, relevant inspection results and received packaging separately. If particulate or residue limits were specified, obtain the evidence addressing those limits rather than relying on the treatment label.
Can visual inspection detect contamination inside sintered mesh?
Visual inspection can identify accessible, observable deposits, but it cannot establish the condition throughout a multilayer porous wall. Guards, support structures and fine layers can prevent direct examination. Record what was visible and what was inaccessible. Where the intended service requires more evidence, agree an appropriate verification method and its coverage instead of treating an unobstructed outer view as complete inspection.
Is ISO 16232 a universal cleanliness requirement for industrial filters?
No. ISO 16232:2018 addresses particulate-contamination assessment for road-vehicle components and systems and does not provide universal acceptance limits. Its public scope excludes film contamination and non-quantitative visual or cloth-wipe assessment. A project using the standard needs an appropriate application basis, specified edition, suitable method and component-specific criteria. Merely writing its number on a purchase order leaves important questions unresolved.
Should a buyer wipe the media with a white cloth?
Do not use an improvised cloth wipe as a quantified cleanliness assessment. A cloth can leave fibers, disturb deposits or damage delicate structures, depending on the media and handling. If a particular surface check is required, agree its method, permitted materials, location and acceptance basis. Keep it separate from any particulate analysis and avoid assuming that a visually clean cloth proves an acceptable element.
What if the protective bag is torn but the filter looks clean?
Document the damage before disturbing the package and hold the affected item for the required review. A clean appearance does not establish what exposure occurred or whether hidden contamination is present. Check which protective barrier was specified, the likely exposure and the application requirement. Release, further inspection, authorized cleaning or rejection should follow a documented decision rather than appearance alone.
Does every dark mark mean corrosion or failed cleaning?
No. Appearance alone may not distinguish a shadow, surface stain, heat-related discoloration, deposit or corrosion. Record the location and appearance and compare them with the agreed condition. Seek technical clarification where the mark is unexplained or relevant to service. Do not label it harmless solely because it is small, or identify its chemistry from a photograph without supporting evidence.
Should the element be cleaned again before installation?
Follow the agreed delivery and installation requirements. Automatic recleaning can introduce contamination, affect seals or disturb the evidence of an as-received problem. Where cleaning is required or authorized, confirm compatibility with the complete assembly and define the subsequent acceptance checks. Preserve the appropriate protection afterward. Cleaning is a controlled action with a verification requirement, rather than a substitute for resolving an unclear condition.
What should be requested from SINFT for a cleanliness-sensitive order?
Provide the application, drawing, critical surfaces, contamination concerns, acceptance criteria and packaging requirements. Specify the records and inspection coverage you need, including whether the requirement goes beyond visual assessment. SINFT can review the requested surface-cleanliness inspection scope with the order. Any specialized quantitative analysis, cleaning qualification or regulated-service requirement must be confirmed separately rather than assumed from the product material or photograph.
Final Thoughts
Accepting a filter element requires a clear link between the service requirement, received condition and supporting evidence. Inspect before disturbing the package, record access limits and resolve unexplained contamination before installation. For a new or replacement order, give SINFT the drawing, application and cleanliness expectations early so inspection, documentation and packaging can be reviewed together and agreed for the actual assembly.